


Soft drinks production plant
 Customer
This Puerto Rico-based beverage company specializes in the production and bottling of soft drinks. Its operations involve high production volumes and demand rigorous standards for hygiene, repeatability and process control.
Although the company had significant experience in bottled water production, it was relatively new to carbonated beverage manufacturing. They therefore sought a supplier with strong industry expertise and the ability to tailor the solution to the project's specific requirements.
 Project
They required an automated facility for the production of syrup concentrate and the final product.
The installation had to provide precise ingredient dosing, optimise cleaning routines and improve traceability ensuring consistent product quality and top hygiene conditions throughout the facility. In addition, a more robust, scalable solution was required, ready to support production growth and move towards a more complete automation environment.
“The INOXPA solution has allowed us to automate the process and ensure constant quality in our production.”
“The INOXPA solution has allowed us to automate the process and ensure constant quality in our production.”
 Why INOXPA?
The customer chose INOXPA because of its ability to provide a fully integrated turnkey solution adapted to the requirements of the mix preparation process in the beverage industry.
 INOXPA solution
The design combined specialised process engineering, hygienic equipment, production automation and proven experience in similar projects with the integration of CIP systems.
This approach allowed the preparation, storage, dosing and cleaning stages to be incorporated into a single facility to ensure more efficient, safe and coordinated operations.
 Installation characteristics
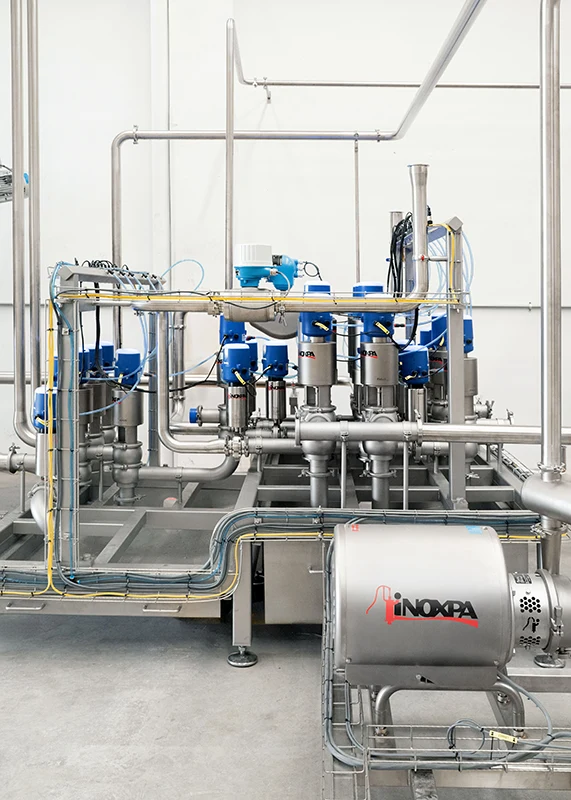
INOXPA designed and supplied a complete line for beverage production, consisting of the following:
- Reactor for syrup concentrate production, featuring water and fructose measurement and dosing systems.
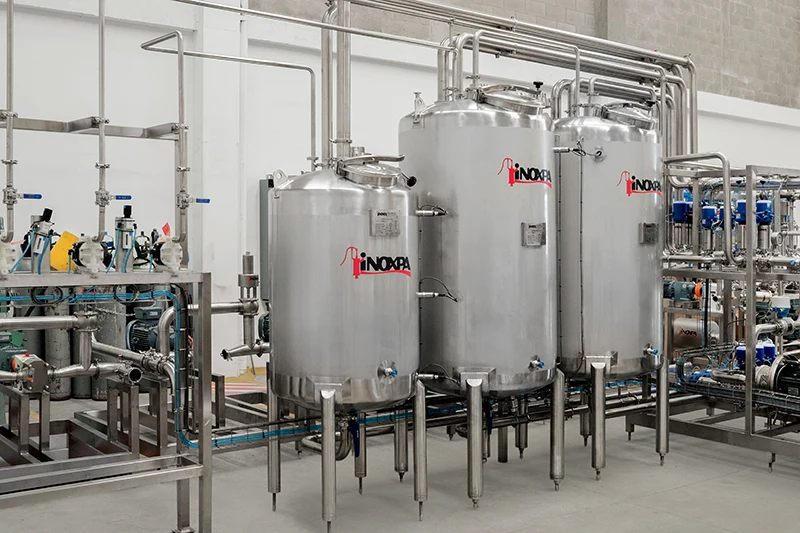
- Two 5000 L finished syrup storage tanks made of AISI 316L, fitted with side-entry agitator systems.
- Pumps for product transfer and dosing into the filling system
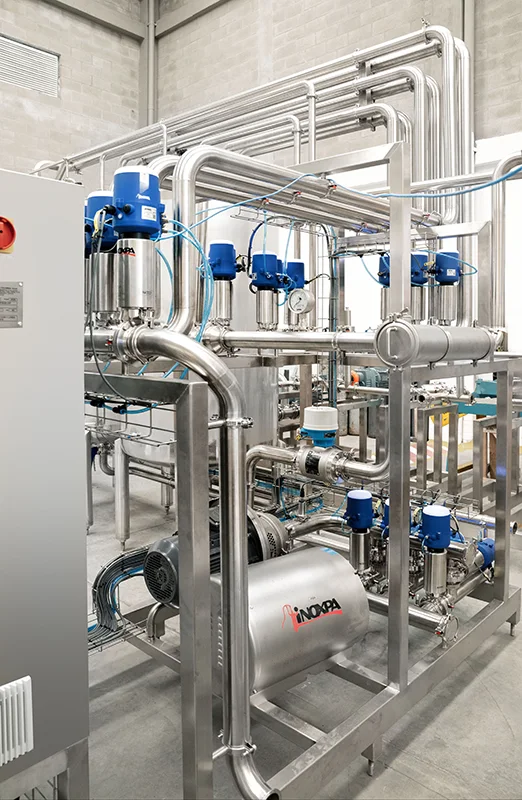
- An automatic 4-tank CIP system, including pumps, hygienic valves and instrumentation to ensure effective and repeatable cleaning cycles.
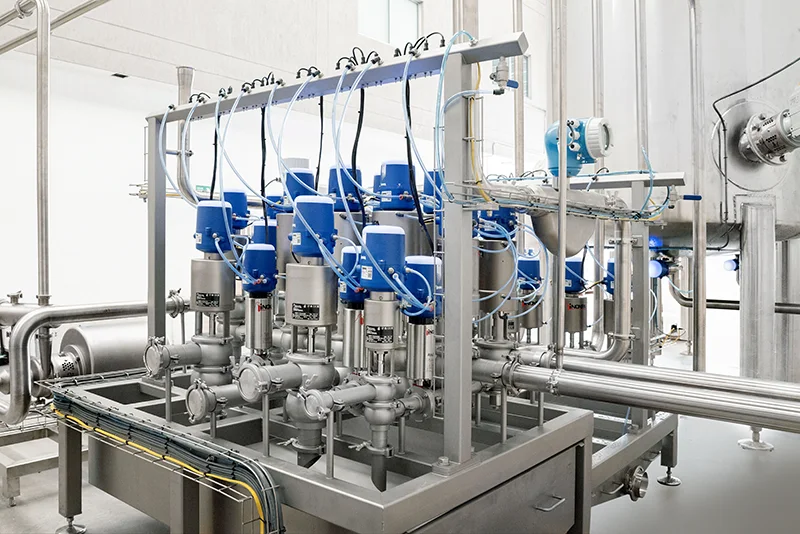
- Valve manifolds for process flow management and CIP solution distribution.
- Fully integrated PLC automation system, ensuring precise control of valves, flow rates, levels, temperatures and cleaning cycles.
 Special features
Thanks to the solution developed by INOXPA, homogeneity and repeatability were achieved in both syrup preparation and the subsequent production of carbonated soft drinks. Cleaning times and production downtime were reduced, resulting in a more efficient plant and enhanced food safety through the CIP cleaning system.
The facility is scalable and therefore prepared for future capacity expansions in response to the growing demand for their products.
The project enabled the company to optimise their production process, improve the final product quality and increase the operational reliability of the plant.
Request information
Soft drinks production plant

